Egg traceability at tens of thousands of eggs a day is decided by one thing: whether the code on the shell can be tied back to a batch you can name. Printing is the easy part; getting the right code onto the right tray, every tray, without stopping the grader is the hard one. Here is how the chain is built.
Egg traceability is not a printing feature. It is a record that happens to be stamped on an egg.
Before a head fires, three things have to exist: a batch identifier for the flock and the day, a plant or farm code that says where the eggs were graded, and a date format that every buyer in the chain reads the same way.
If those three are agreed verbally at the start of a shift, the code on the shell is decoration. If they arrive as a job preset, it is a record.
Most codes carry more than buyers ask for and less than a recall would need. Four fields earn their place.
| Field | Who reads it | When it gets read |
|---|---|---|
| Pack date | Retailer and buyer | At goods-in, and again on the shelf |
| Lot or batch | You, during a recall | When one pallet has to be separated from the rest |
| Farm or plant code | Inspector and buyer | On a spot check, or a complaint |
| Best before | Shopper | At the point of purchase |
Everything beyond those four competes for the same character height. A fifth field usually means all five get smaller.
The usual worry at this volume is that traceability coding will slow the line. It rarely does, because the coding station sits in a gap the grader already leaves.
A six-nozzle bar over the conveyor codes a full 5×6 tray in one pass at 20 trays per minute. The tray is never broken apart, so no egg is re-handled just to be marked.
The station arrives as one frame: conveyor, retaining baffles and head bar together. Alignment survives a wash-down, which is what keeps the code in the same place on the ten-thousandth tray as on the first. Specifications are on the six nozzle egg coding machine page.
A code only traces if someone can go from shell to record. The printed string has to appear somewhere else as well: a packing log, a spreadsheet, or the machine’s own job history.
Interfaces decide how easily that gap closes. USB and RS232 let a job arrive as a file, so the same string exists in the office and on the shell without anyone retyping it.
The batch changes and the code does not. A new flock, same date format, nobody updates the lot number. Every egg after that point traces to the wrong batch.
Two batches share a line. If a tray of older eggs goes through between two fresh ones, the code is right for one tray and wrong for the other, and nothing on the shell shows which is which.
Reprints go unrecorded. A jammed tray is pulled, fixed and sent through again. Now two eggs carry the same code and the record has no way to explain it.
None of these are printer faults. All three are handover habits, which is why the shift change matters more than the head.
The first is who reads the code. A retailer reading a date on a shelf needs legibility at arm’s length. An inspector reading a plant code needs accuracy, not size.
The second is how far back you need to go. Day-level needs a date, batch level needs a lot number, and egg traceability at shell level needs a serial on every egg with a database behind it.
Most farms selling into wholesale run egg traceability at batch level and stay there. Egg level is an export and premium-retail requirement, and it changes the machine class, not just the code layout.
The US federal rules on egg inspection describe what records a handler is expected to keep, which is the reference buyers tend to quote. It is set out in 9 CFR Part 590.
Other line layouts and coding sequences are collected under our coding solutions.
Same factory, four jobs. Traceability work tends to land on the mixed-tray machine, because batches change without the tray being sorted.
| Machine | Best for | Speed and resolution | Height | Interface |
|---|---|---|---|---|
 Six Head Egg Inkjet PrinterS10-6 |
High-volume grading lines on standard trays | ≈ 36,000 eggs/hour20 trays/min600 dpi HD | 12.7 mm max | USB / HDMI |
 Six Nozzle Egg Coding MachineS600D |
Mixed tray layouts that must not be sorted | ≈ 36,000 eggs/hour20 trays/min300-600 dpi | 2-12.7 mm | USB, RS232 |
 XY110 Egg Inkjet PrinterXY110 |
Smaller farms, duck eggs and mixed sizes | ≈ 9,800 eggs/hour30 eggs in ~11 s300-600 dpi | 2-12.7 mm | USB, DB9 |
 Small Character Egg PrinterS200PLUS |
20 mm characters, database codes | ≈ 7,200 eggs/hour15 s per traydpi on request | 2-20 mm | USB, RS232, Ethernet |
Hourly figures are calculated from the speed the factory publishes, on a standard 5 × 6 tray (30 eggs). Real throughput follows your line speed, loading and stoppages.
Tell us your daily output and how far back you need to trace, and we will map the code fields to the machine that prints them.
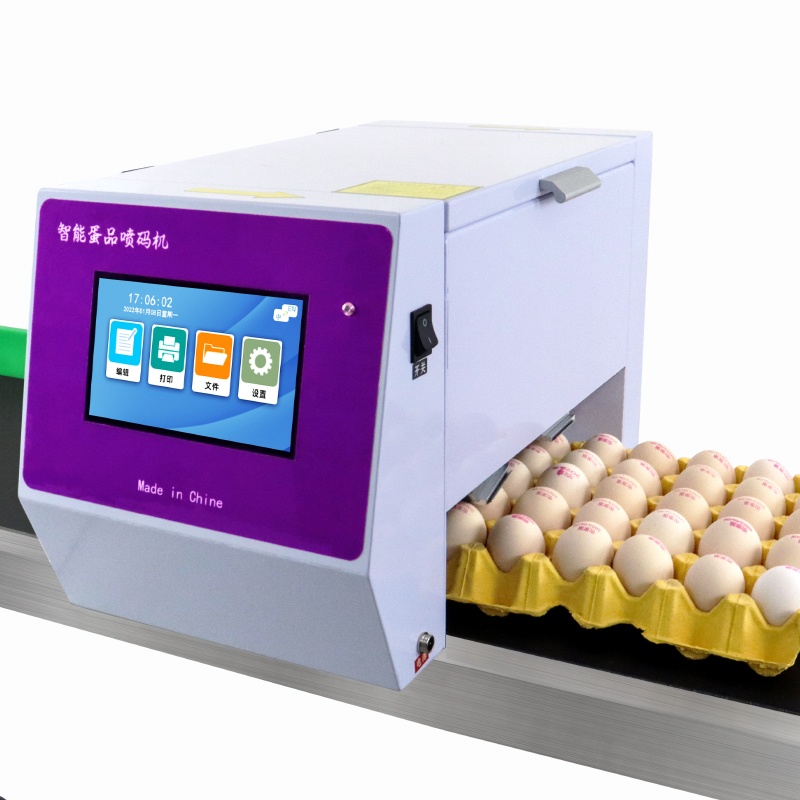
S600D
Six nozzles, one full tray, no sorting needed
SHICAI builds food-grade egg coding machines for poultry farms and packers in the US, UK, EU, Australia and worldwide. Tell us your daily volume and egg types, and our engineers will recommend the right model and send a free sample print.
Tell us about your line — we reply within 24h.